










Who Owns the Complete Result
A GMP facility delivered by five firms leaves the risk with the owner. See how one-source delivery controls design, interface, and commissioning risk.
Executive Summary
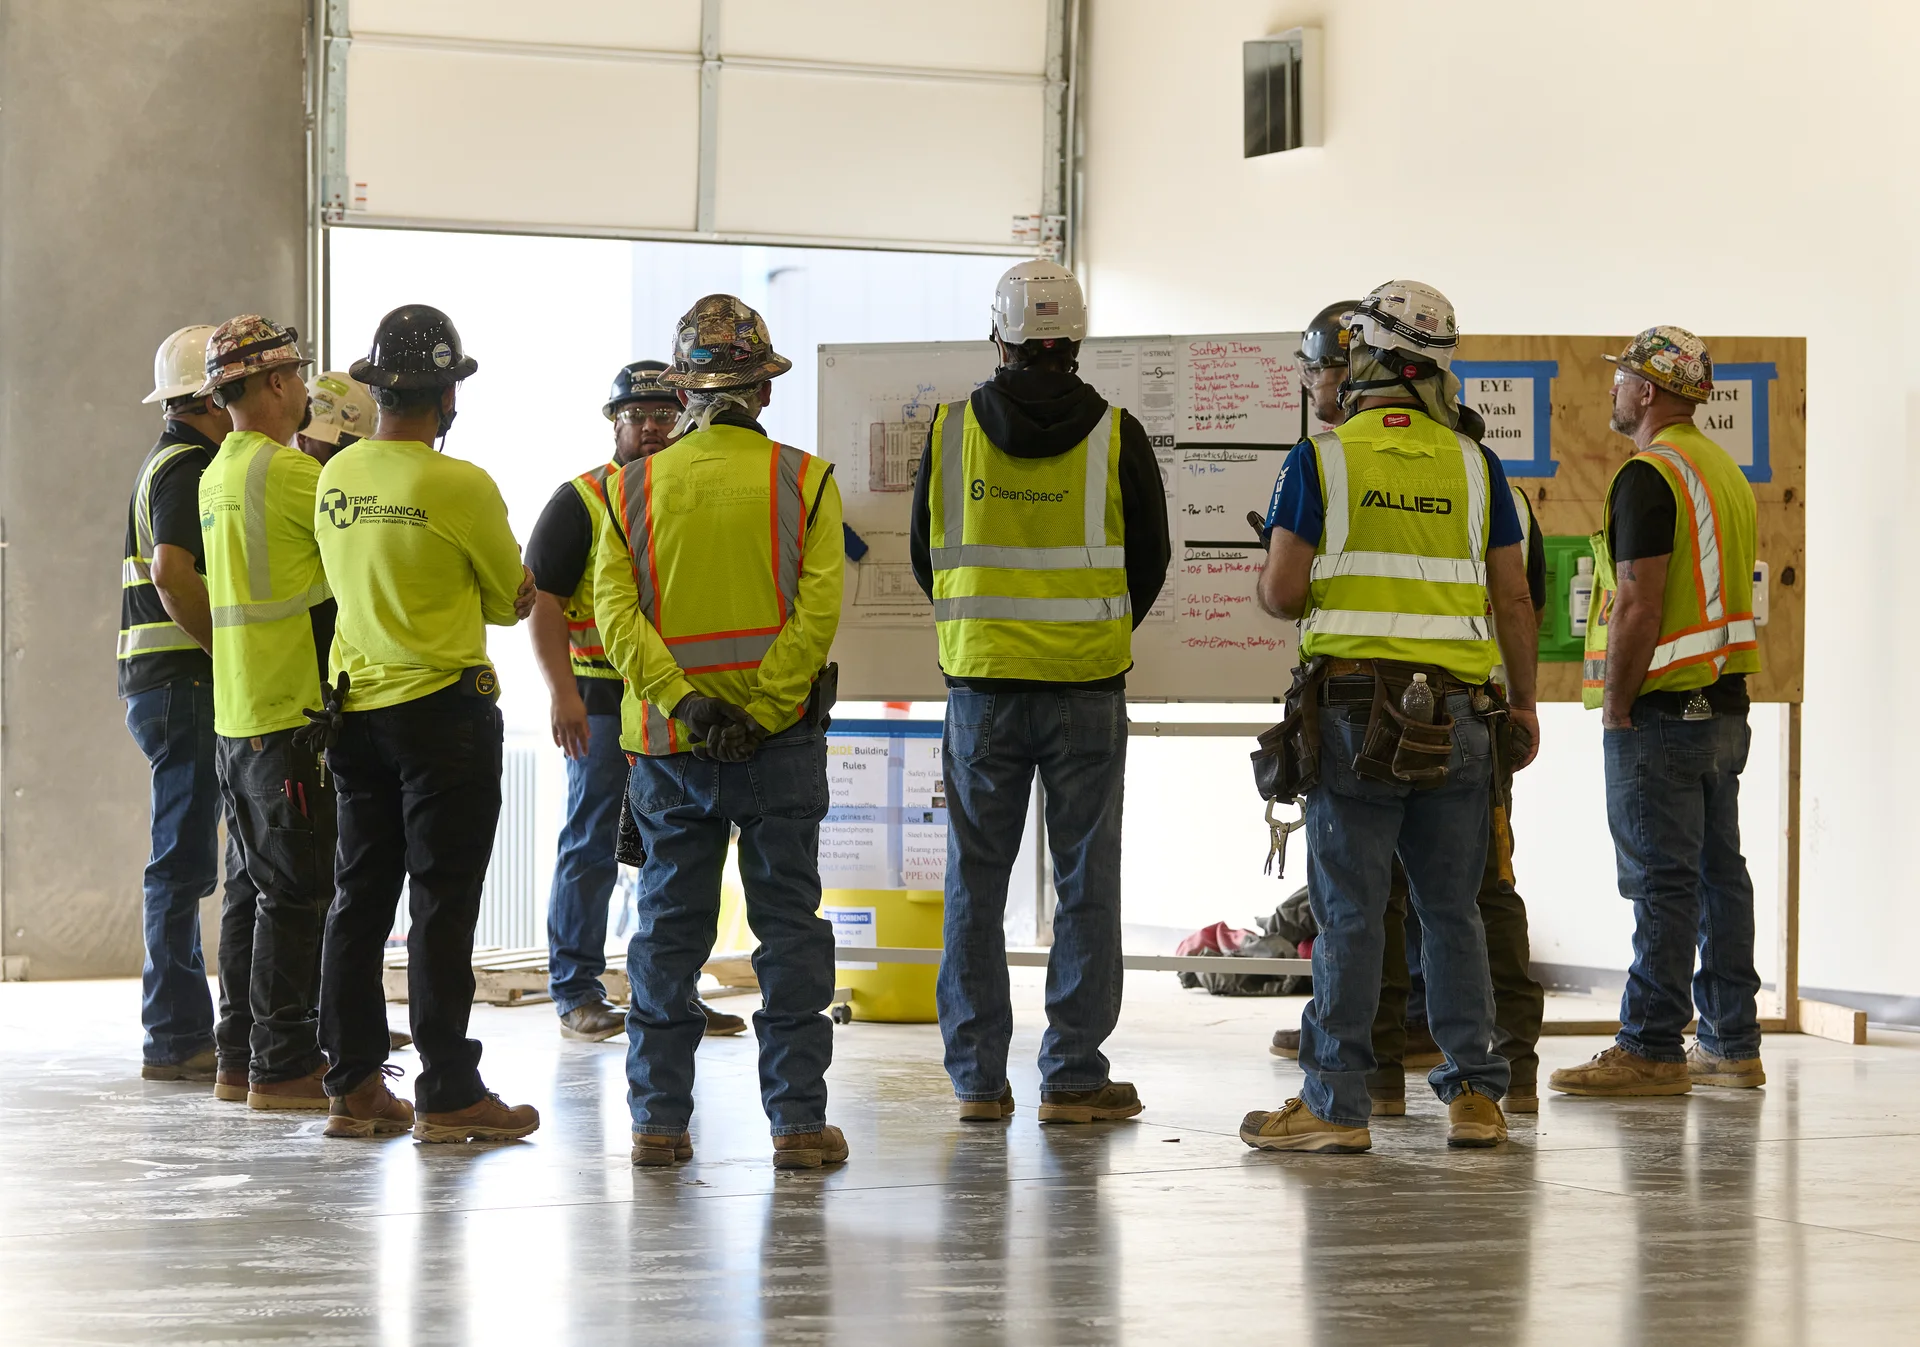
A GMP facility delivered through five or more separate firms is not truly integrated.
The contracts are divided. So are the technical responsibilities, the schedules and the definitions of completion. When something falls between those boundaries, the risk returns to the owner.
That risk does not stop at construction. A delayed qualification, an unresolved interface, a failed test, rework, a change order or a late production start can directly affect commercialization and revenue.
For executive leadership, the real question is not how the facility gets built. It is how much business risk the organization is willing to carry while it is being built. Every unresolved interface is exposure: to capital, schedule, regulatory readiness, labor, inventory timing and the date the facility starts generating revenue.
CleanSpace changes the structure. Facility programming, design, engineering, project controls, procurement, cleanroom manufacturing, construction coordination, self-perform installation, CQV, compliance, service and maintenance all sit under one operating structure.
One source. One technical intent. One accountable organization.
The goal is not simply fewer vendors. It is moving responsibility for integration away from theowner and onto an organization built to manage it.
Design Risk Is Controlled Before Construction
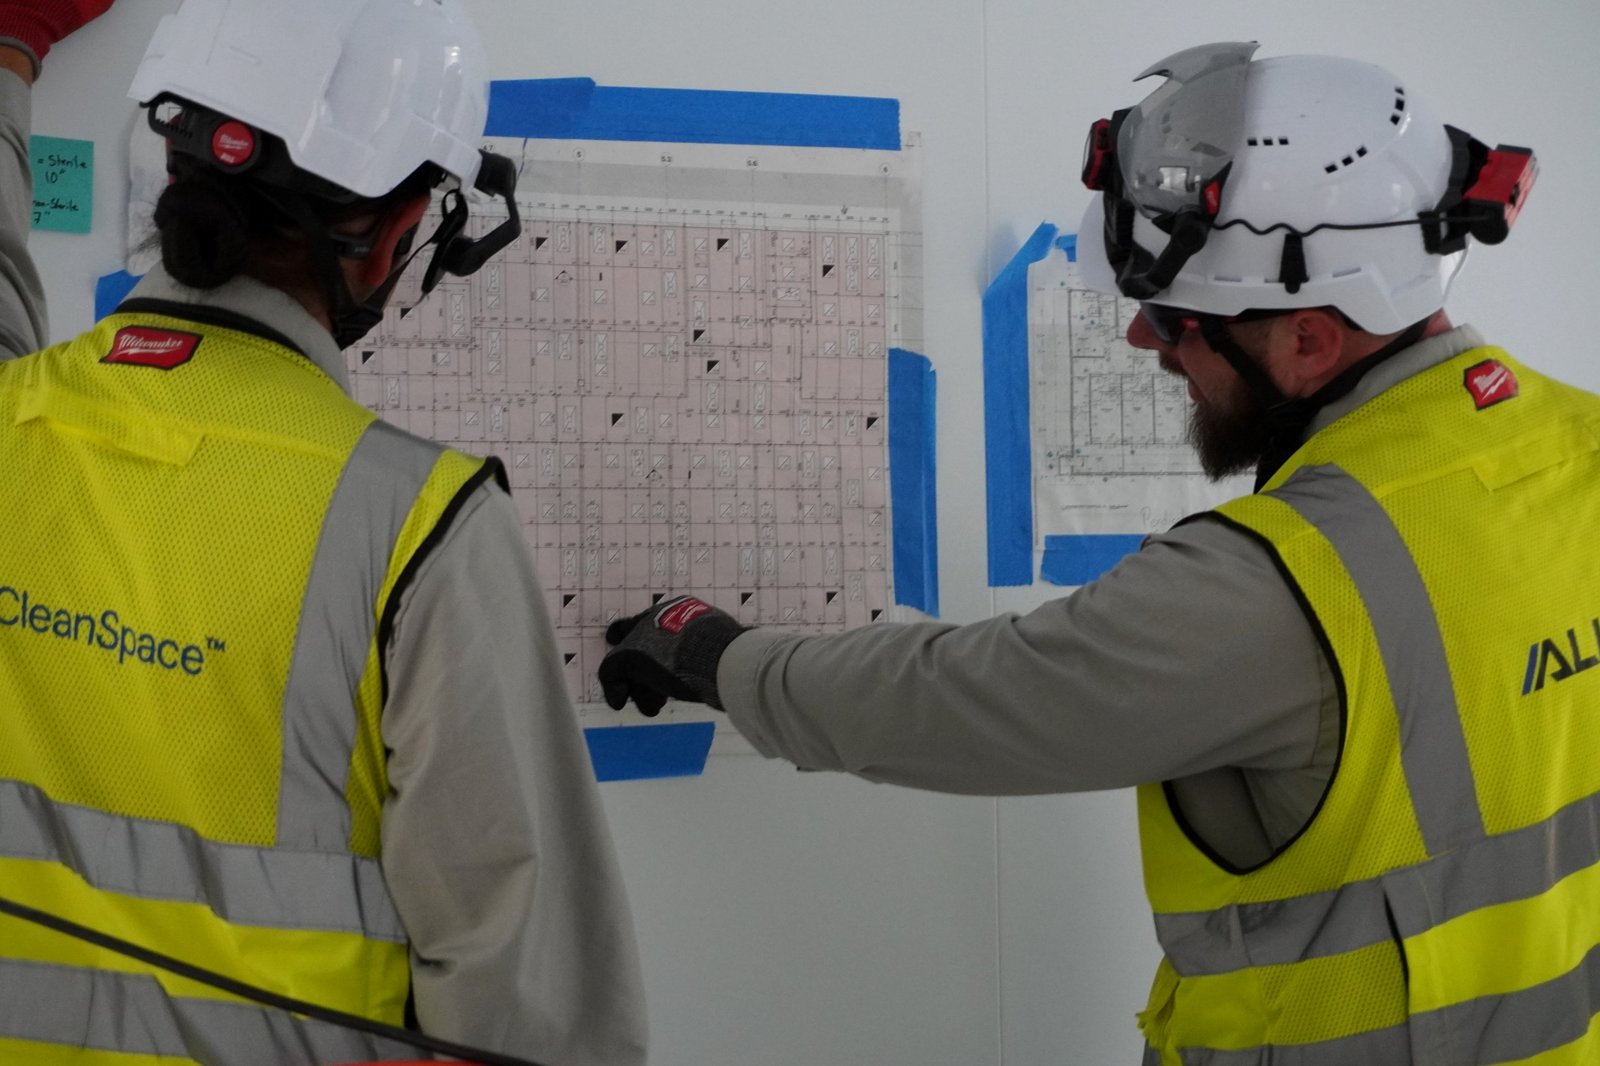
CleanSpace starts with the process requirements that drive the facility. Product flow, personnel flow, material and waste movement, room classifications, pressure relationships, cleaning requirements, equipment, utilities, maintenance access and qualification requirements become the facility program and engineering criteria.
The same organization then coordinates the cleanroom architecture with HVAC, controls, electrical, process utilities, mechanical systems, fire protection, structure and equipment.
That continuity matters. A change to a filling line can affect room dimensions, operator circulation, HEPA coverage, return-air locations, ceiling penetrations, utility demand, structural loading, maintenance access and validation boundaries. In a fragmented model, those impacts pass through multiple consultants, contractors and vendors. In the CleanSpace model, the change is evaluated across the complete controlled environment before drawings are released and materials are manufactured.
For the owner, design becomes a way to protect capital, not just a way to produce construction documents. The earlier an interface, constructability issue or qualification requirement is found, the more options the owner has to fix it without absorbing downstream cost and schedule.
Interface Risk Has One Owner
Cleanroom performance is decided at the interfaces.
- A pressure cascade depends on airflow, room leakage, doors, interlocks, wall joints, ceiling penetrations, utility panels, controls, and balancing.
- A walkable ceiling requires coordination between structure, HEPA filters, lighting, sprinklers, process drops, access, fall protection, and maintenance loads.
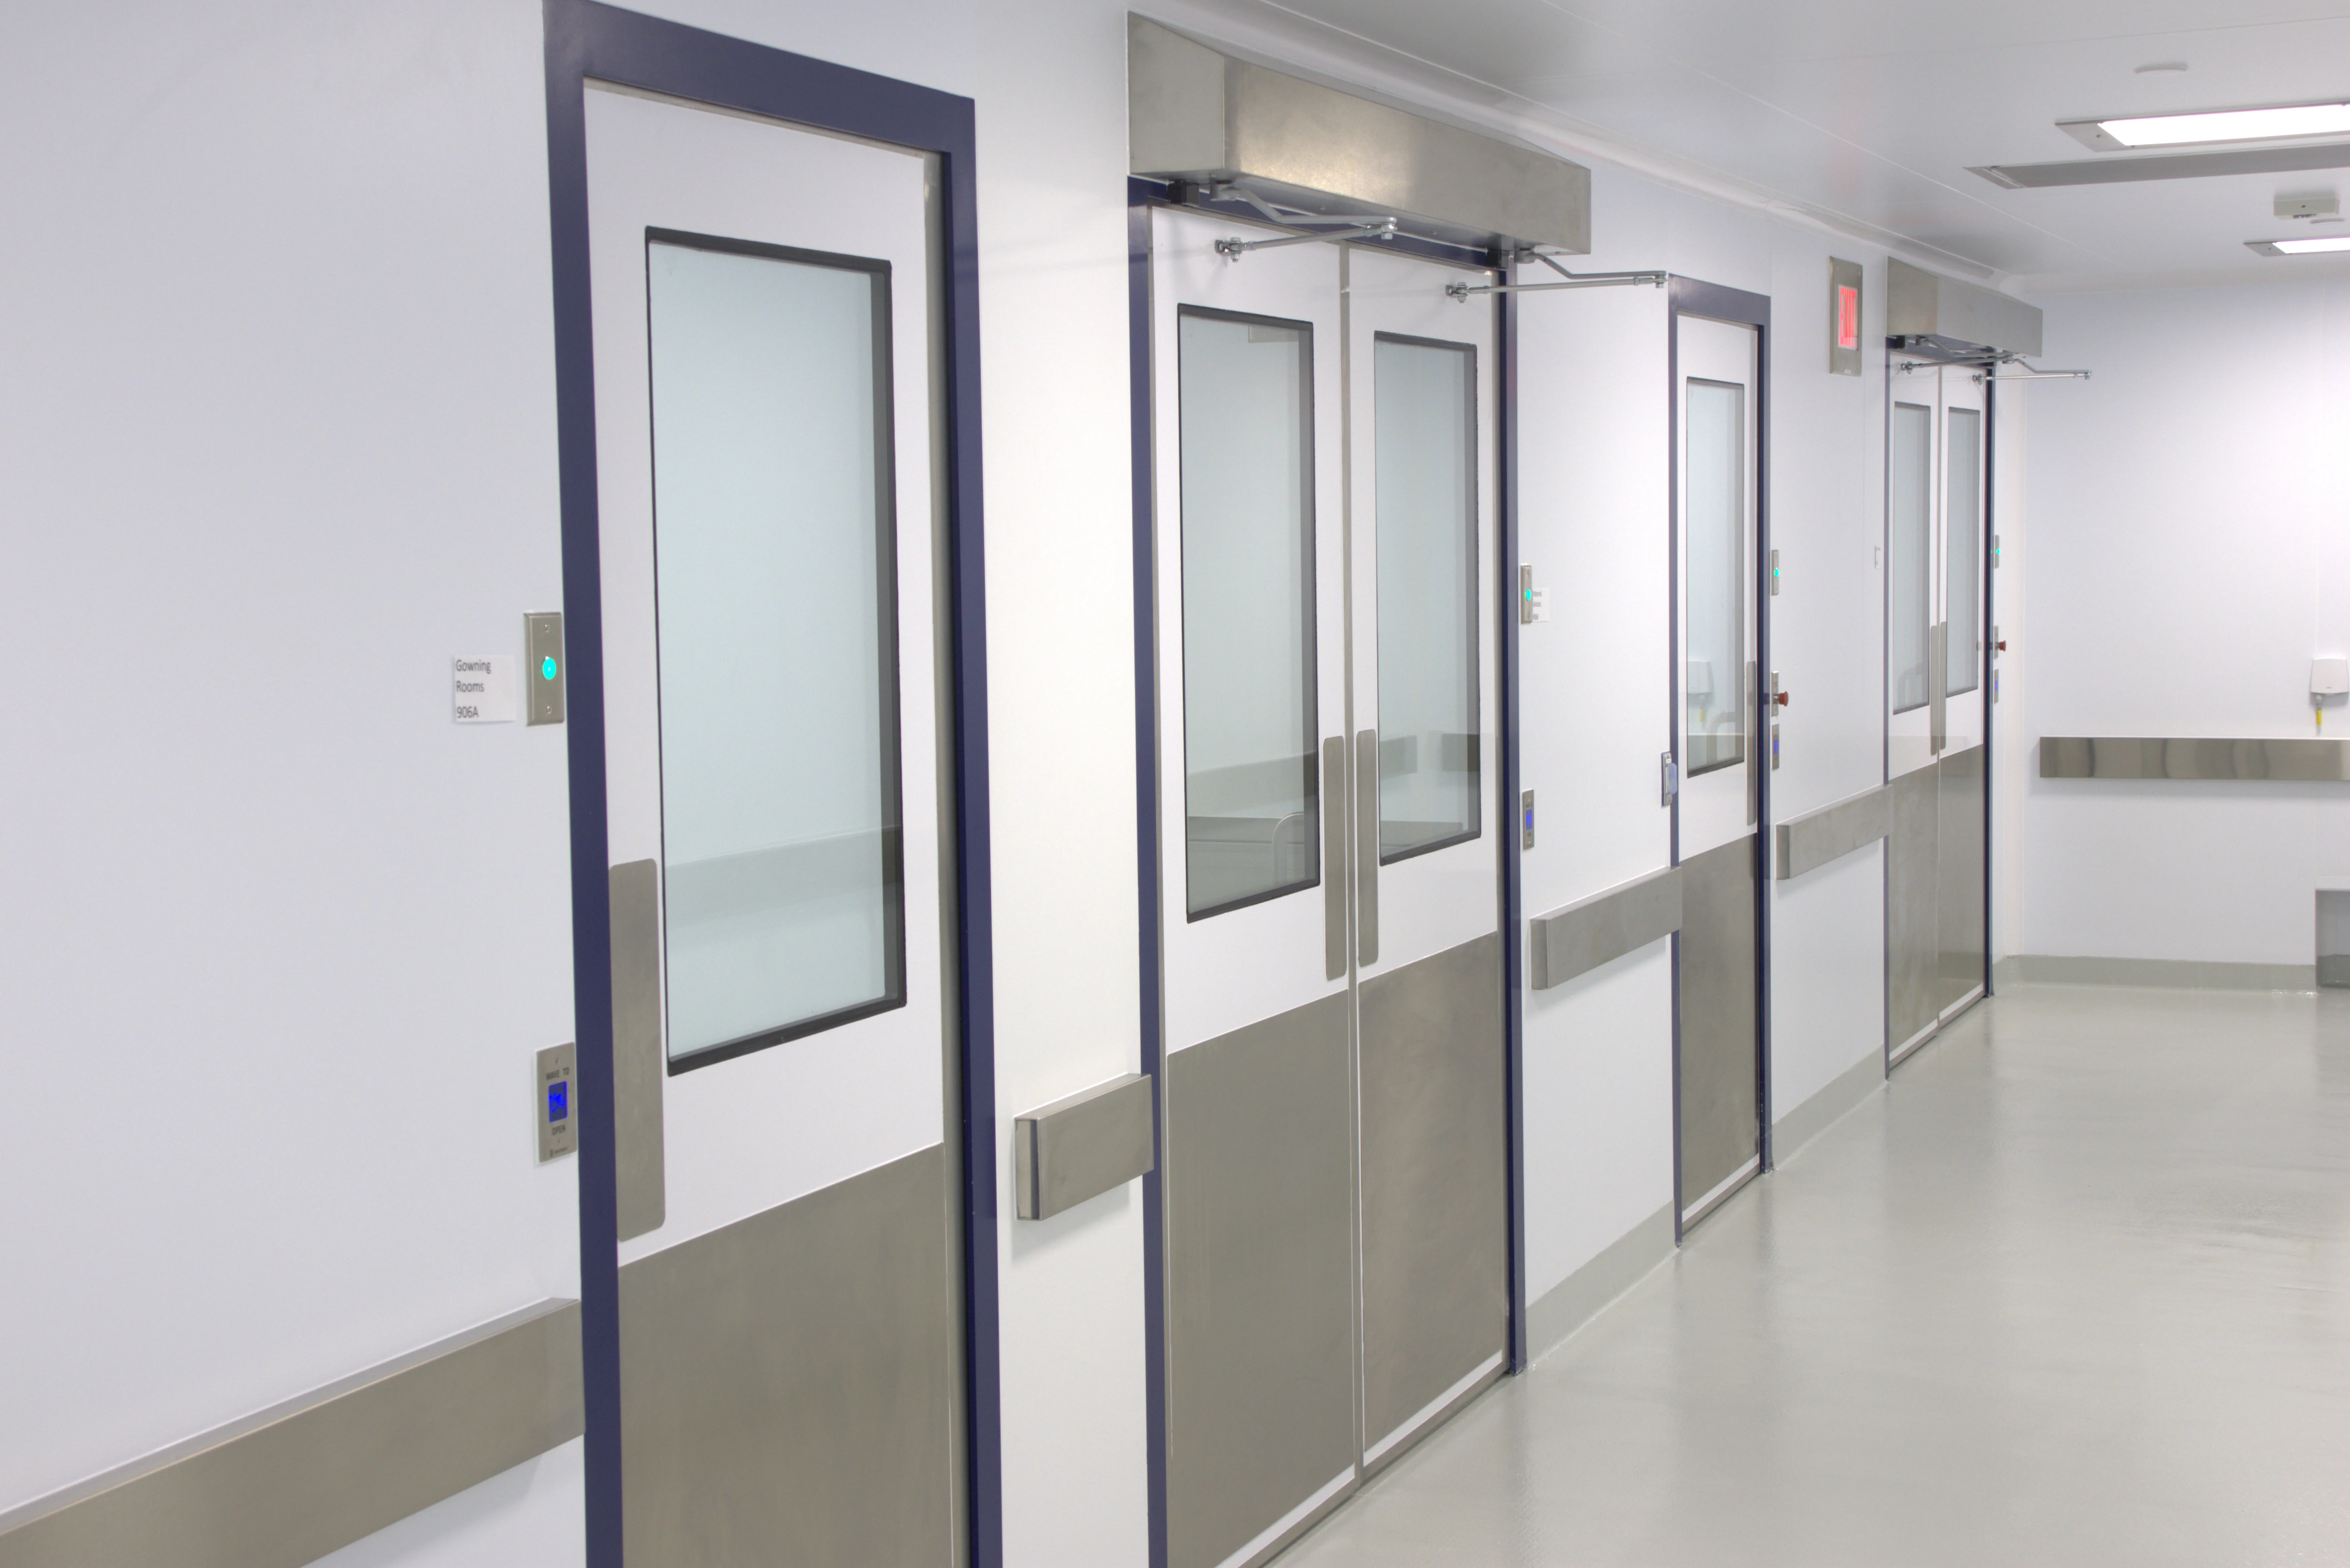
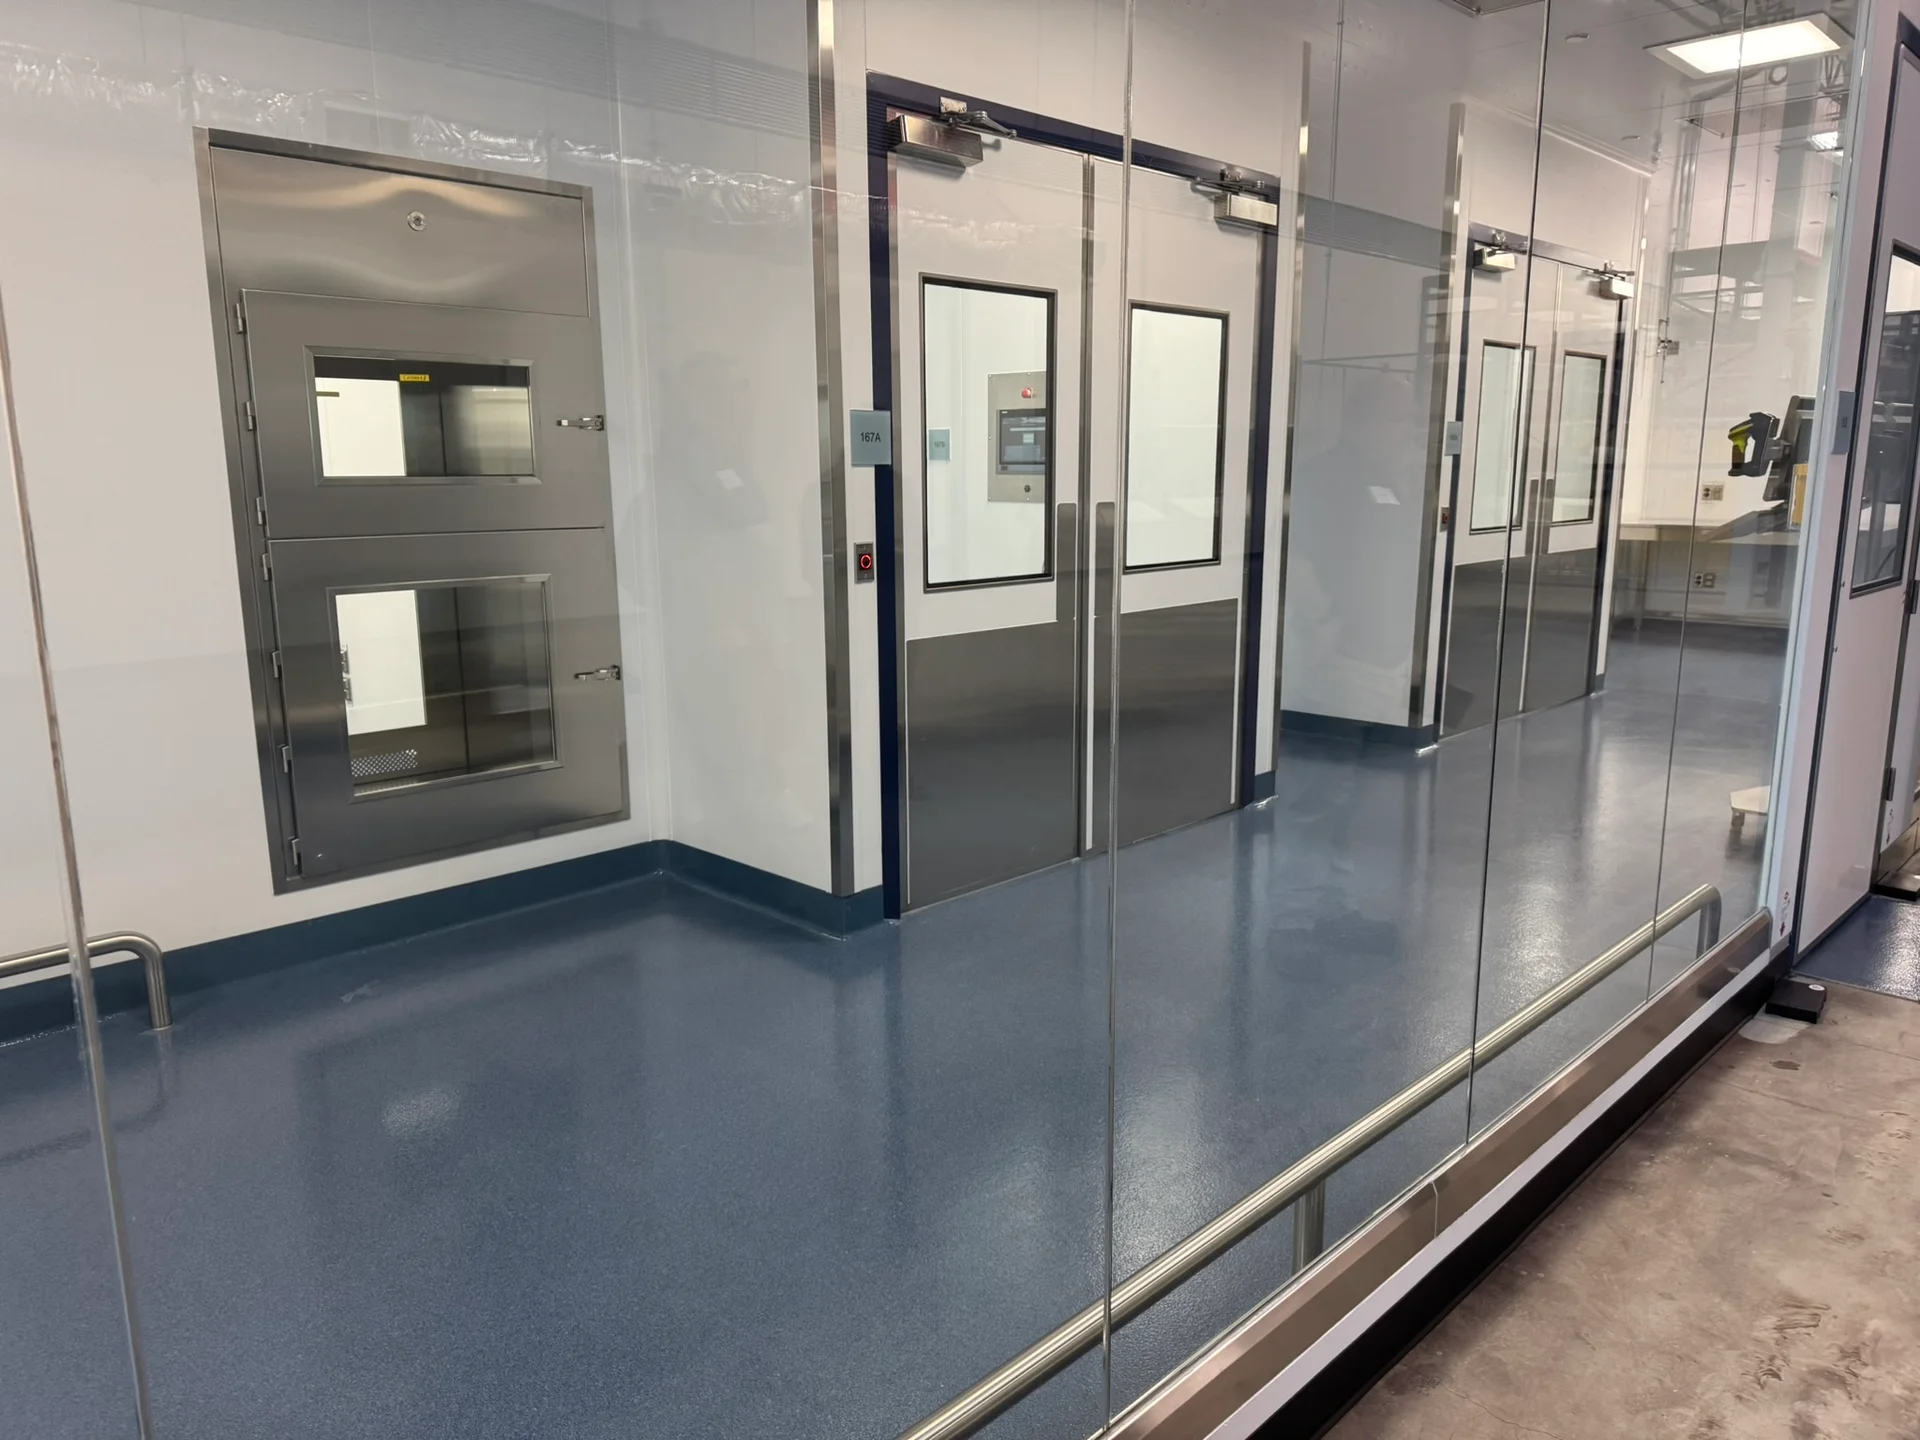
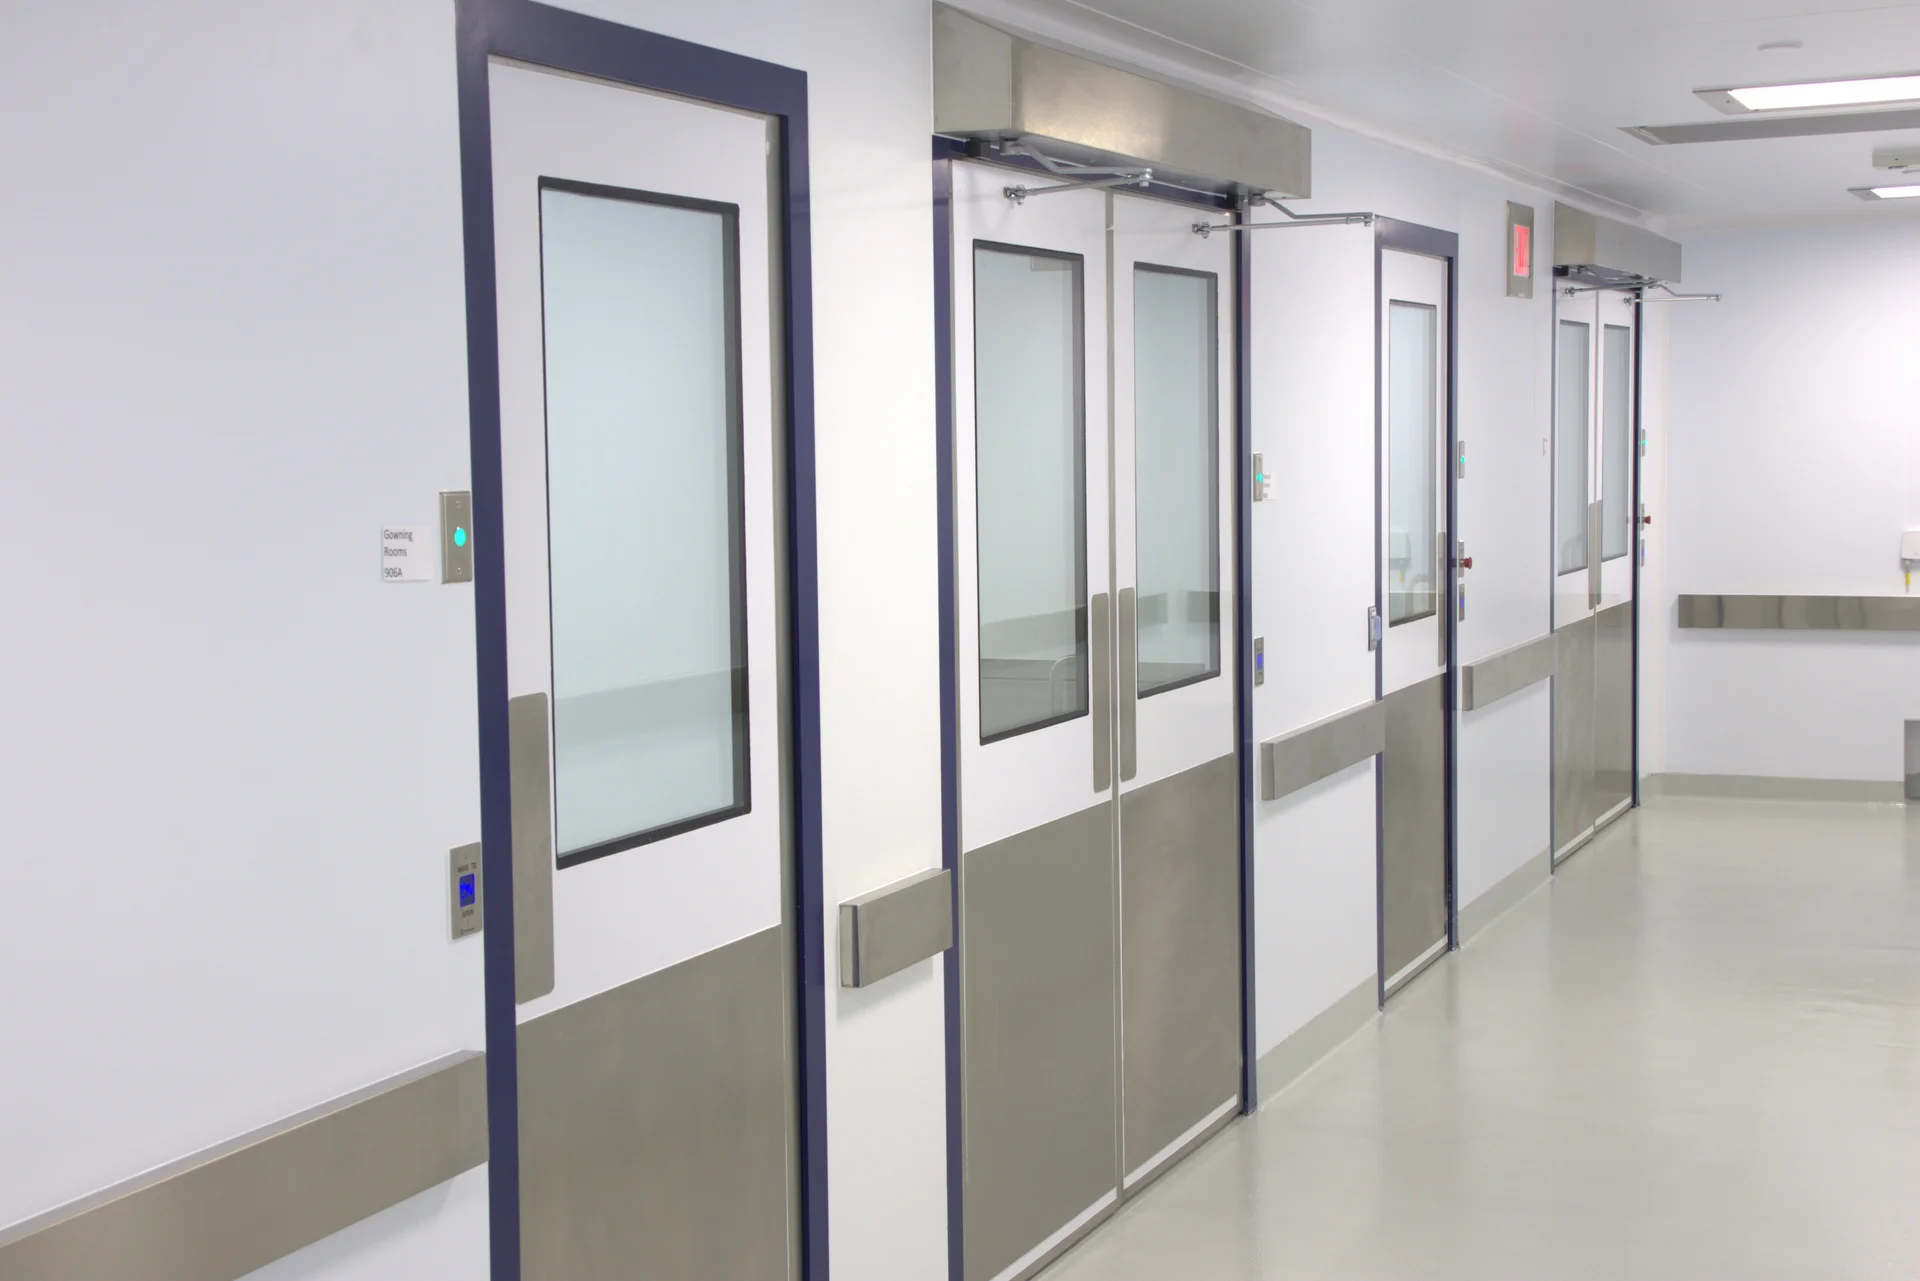
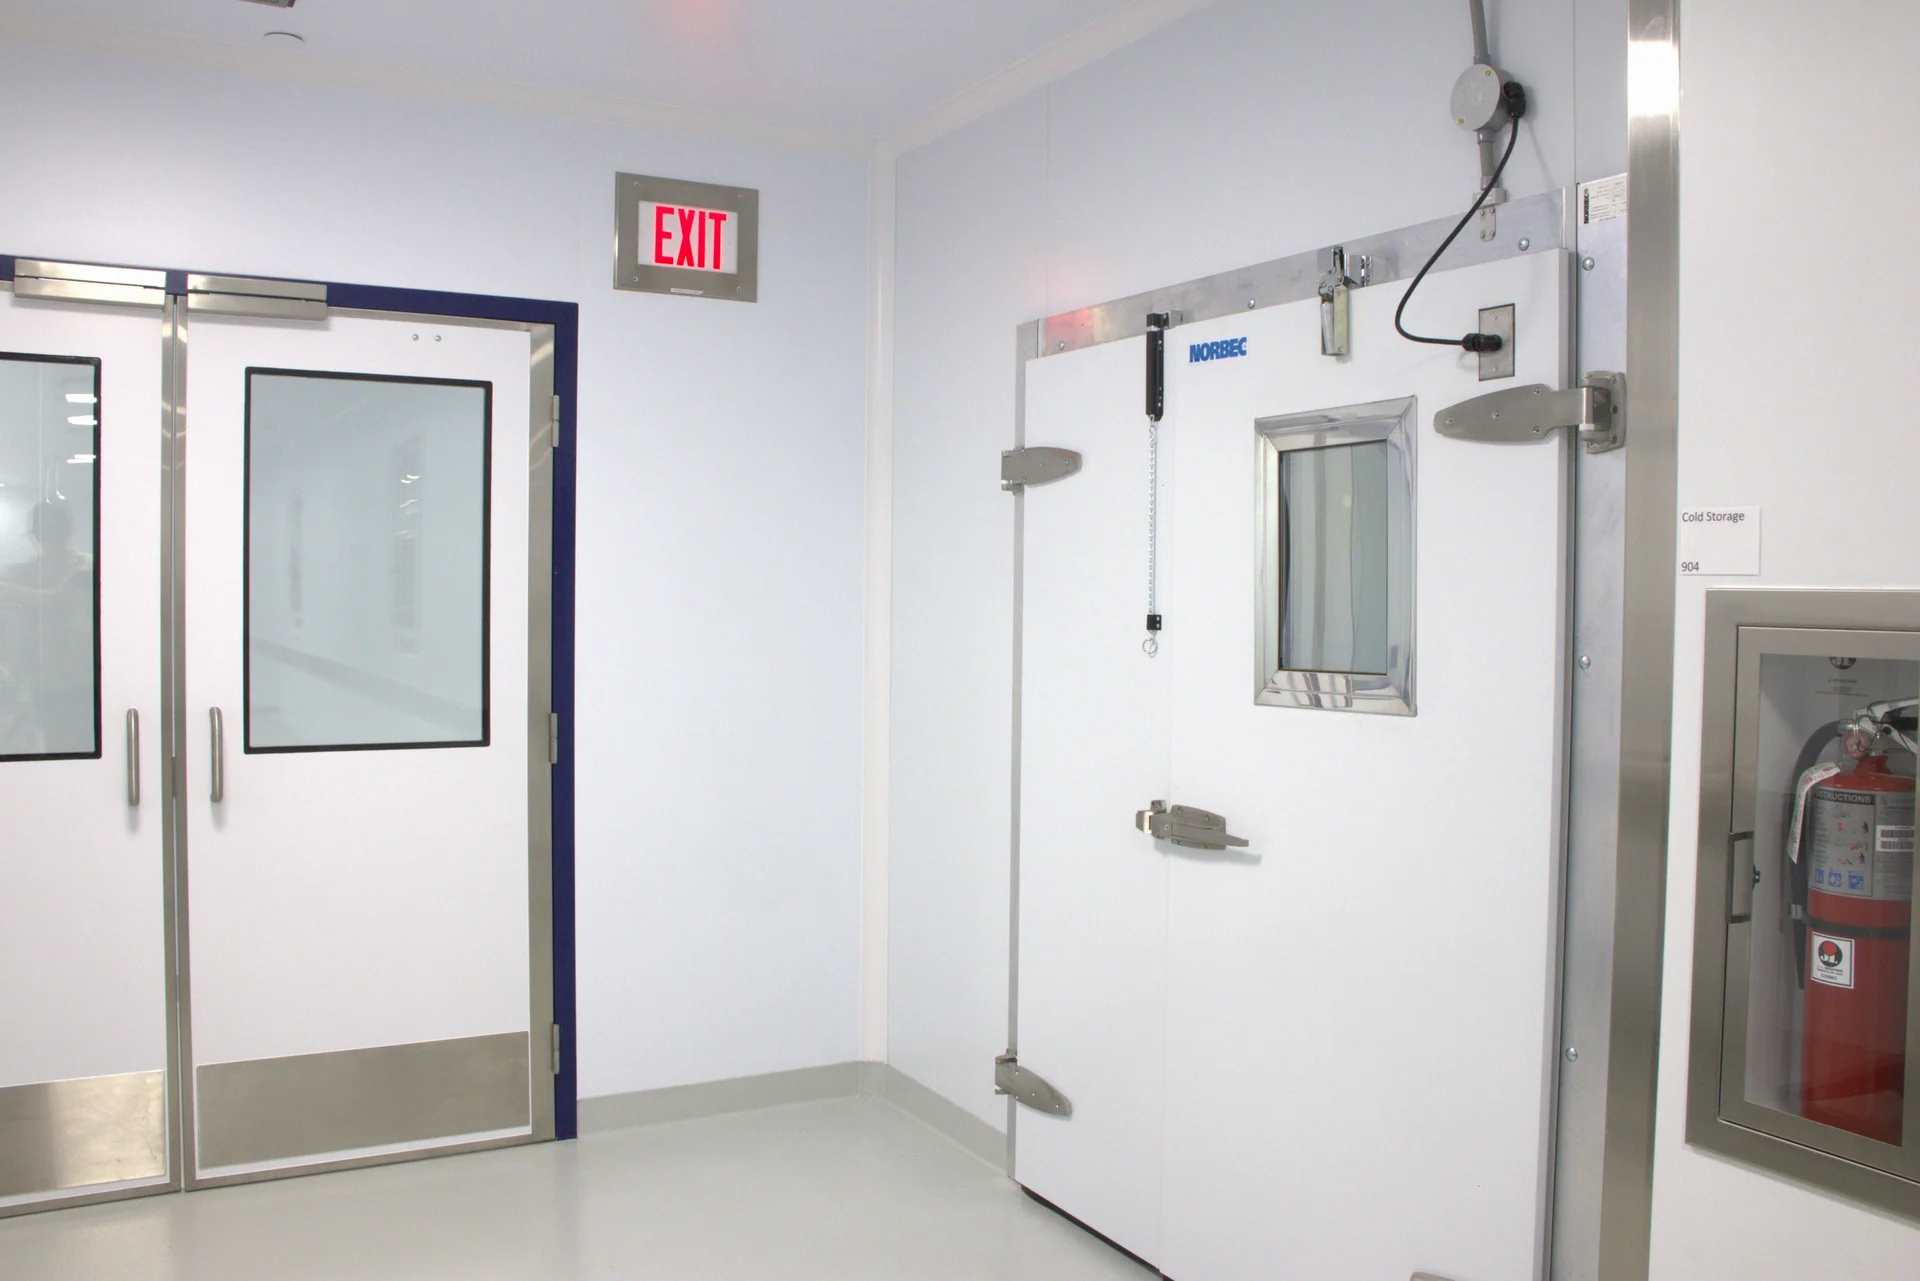
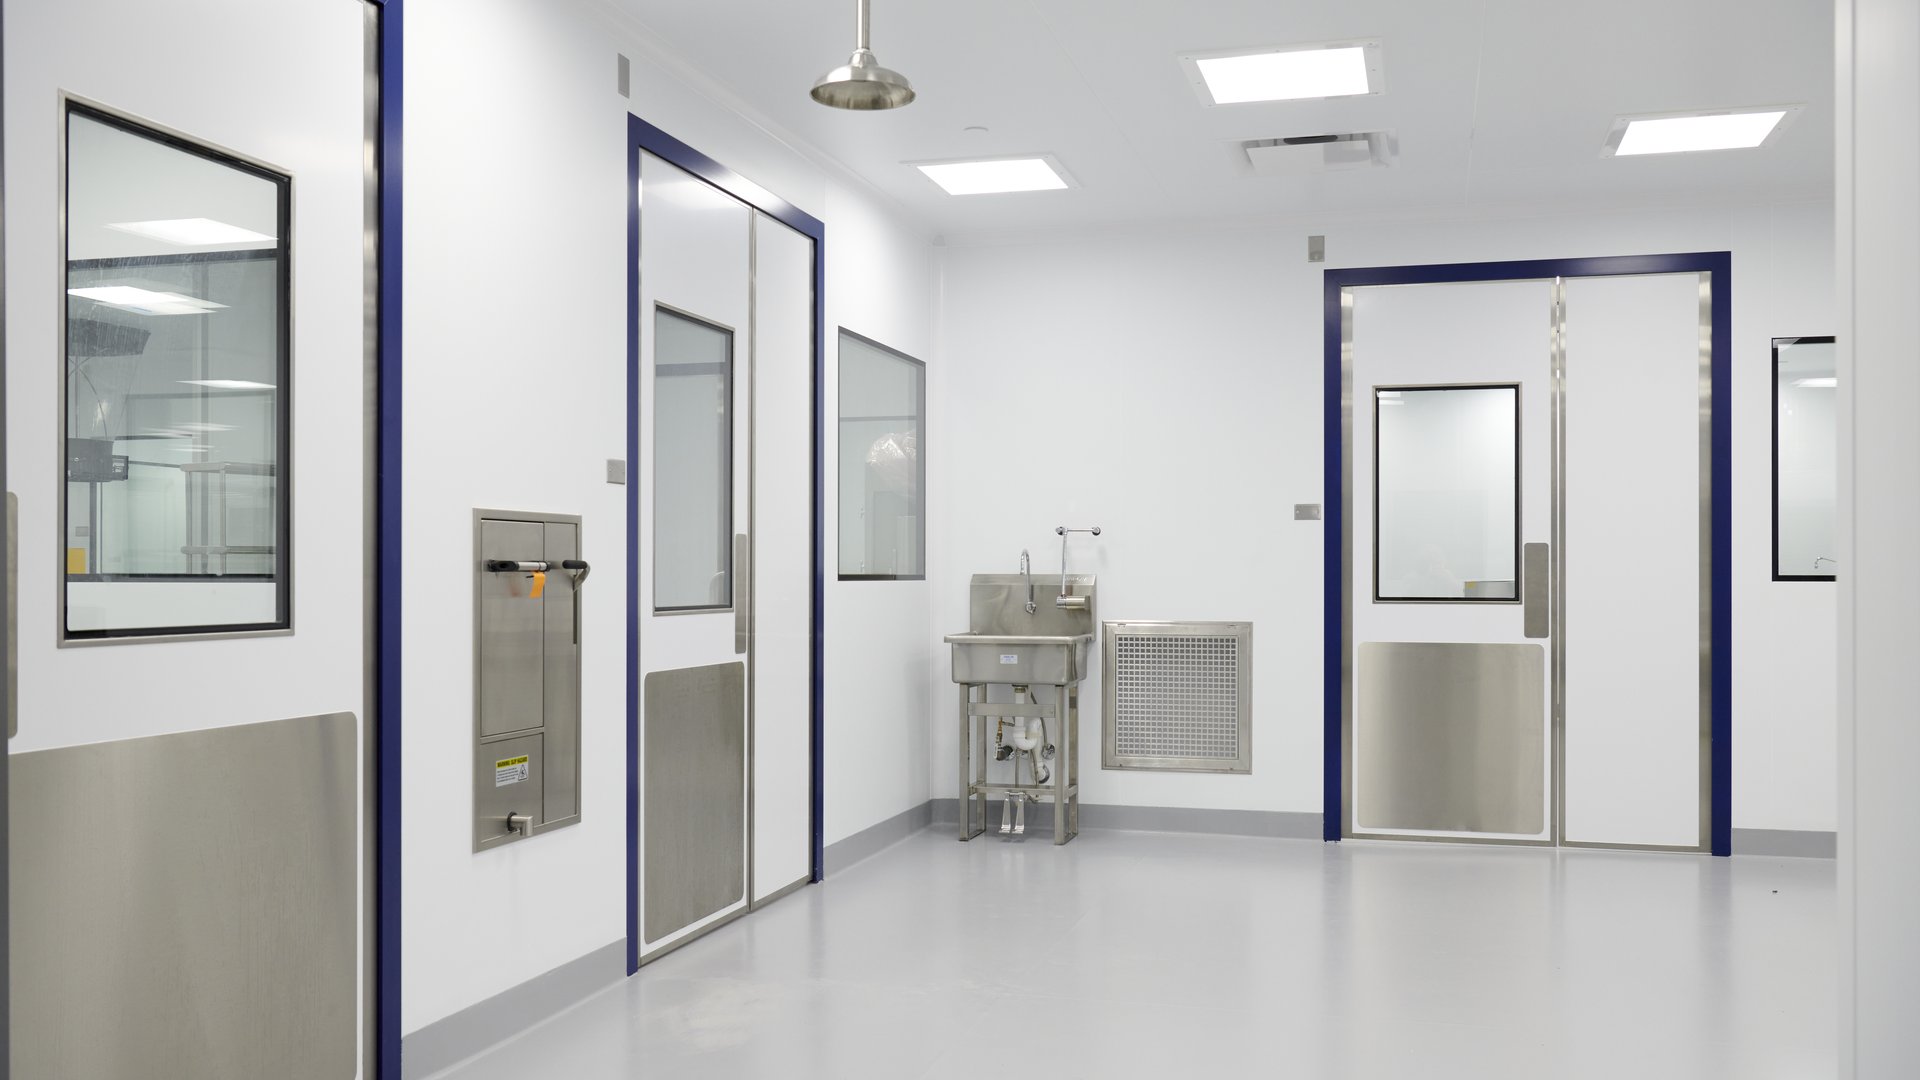
- A cleanroom door brings together the frame, hardware, seals, access control, power, controls, alarms, life safety, and pressure recovery.
These are not independent components. They work as one operating system, and CleanSpace engineers them as connected assemblies. Interface requirements carry through the coordinated model, shop drawings, fabrication, installation planning and commissioning documentation. When a conflict appears, the design, manufacturing, installation and CQV teams resolve it inside the same structure.
The owner does not have to determine which company is responsible for the space between two contracts.
That matters most near startup, when an unresolved interface stops being an engineering issue and becomes a qualification, schedule, labor or commercialization issue.
Manufacturing Risk Is Connected to Engineering
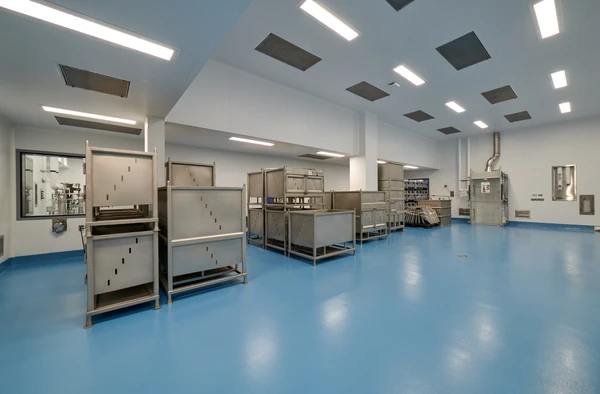
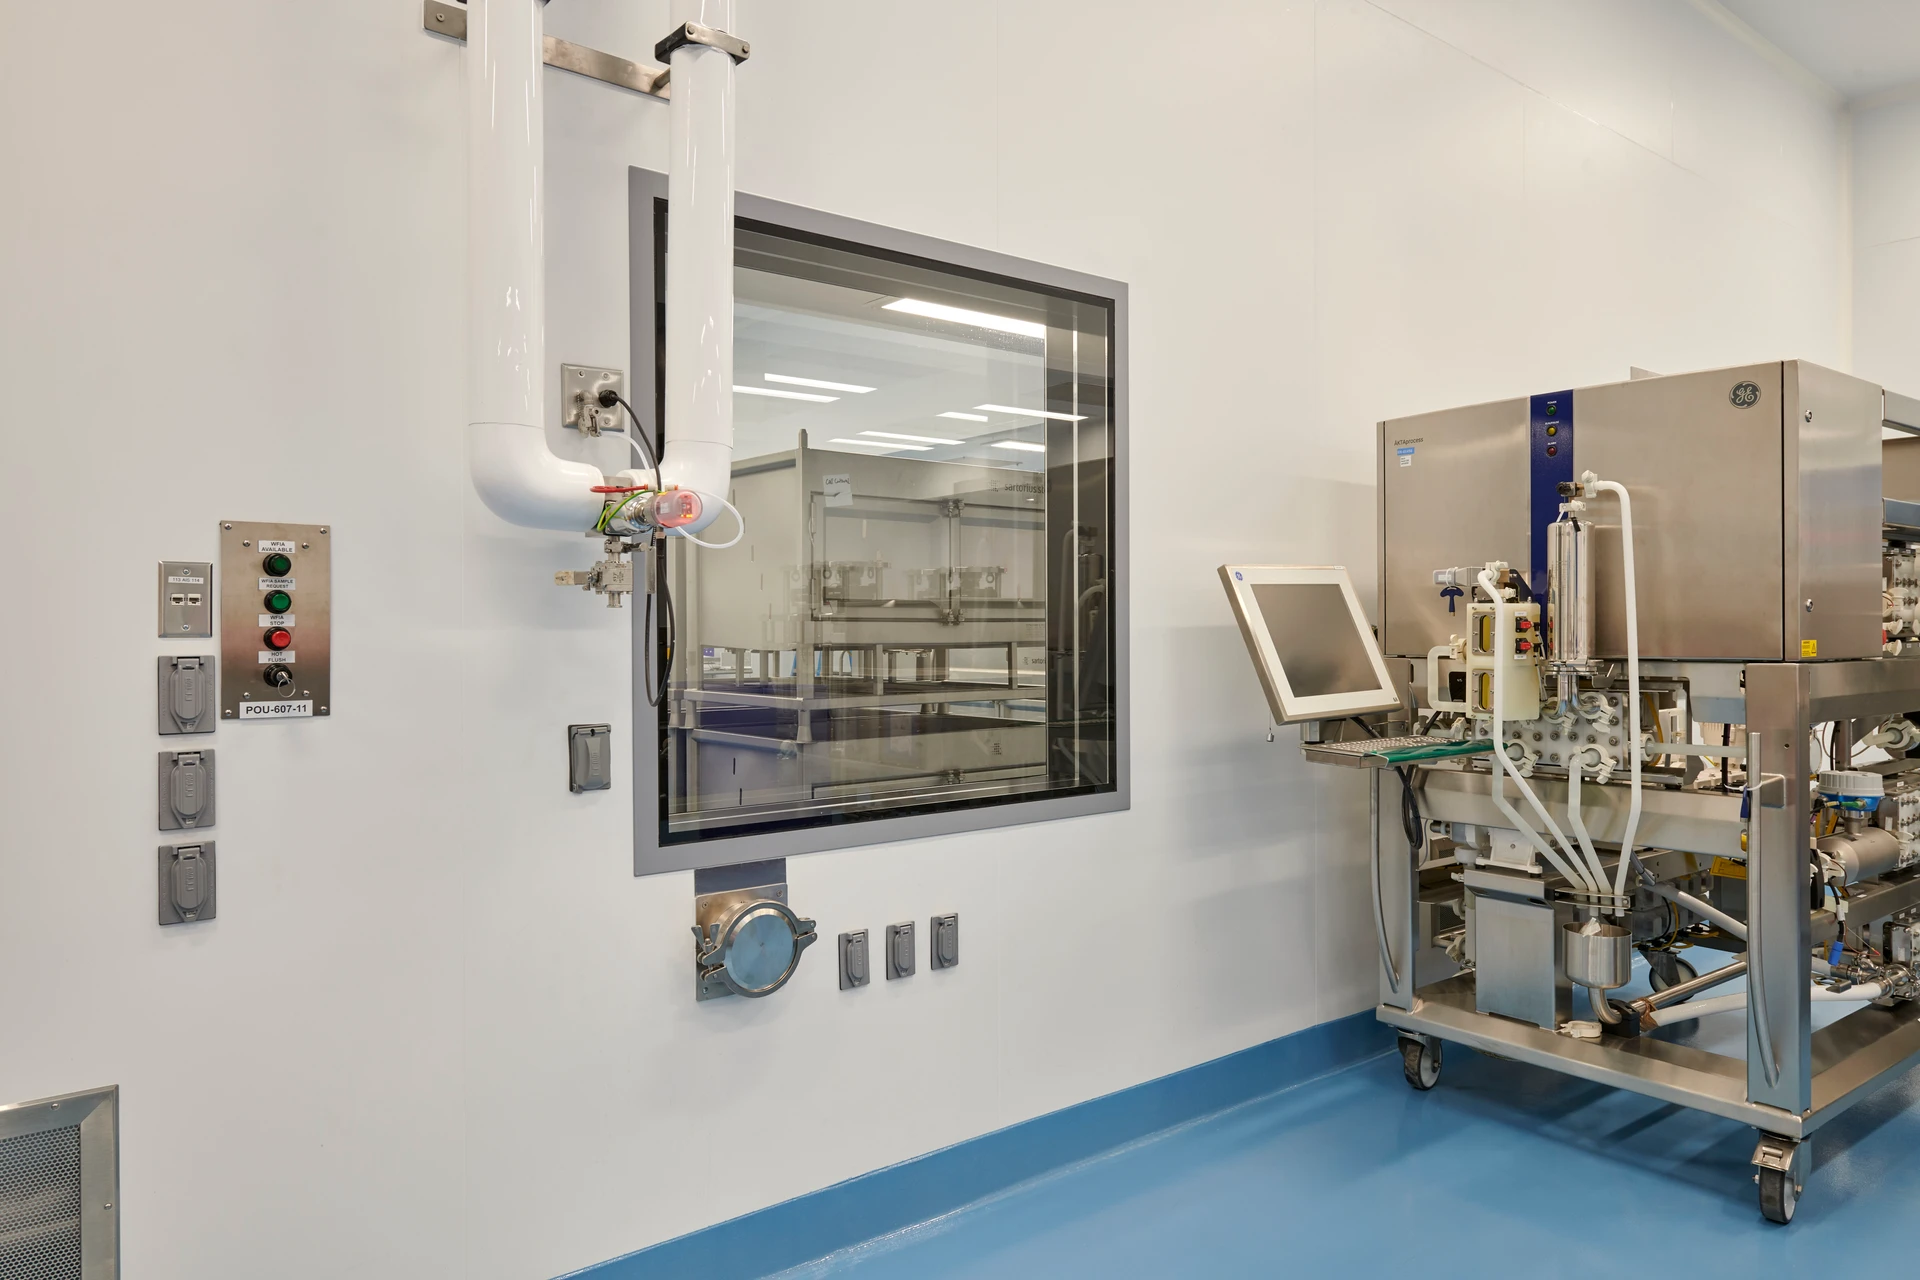
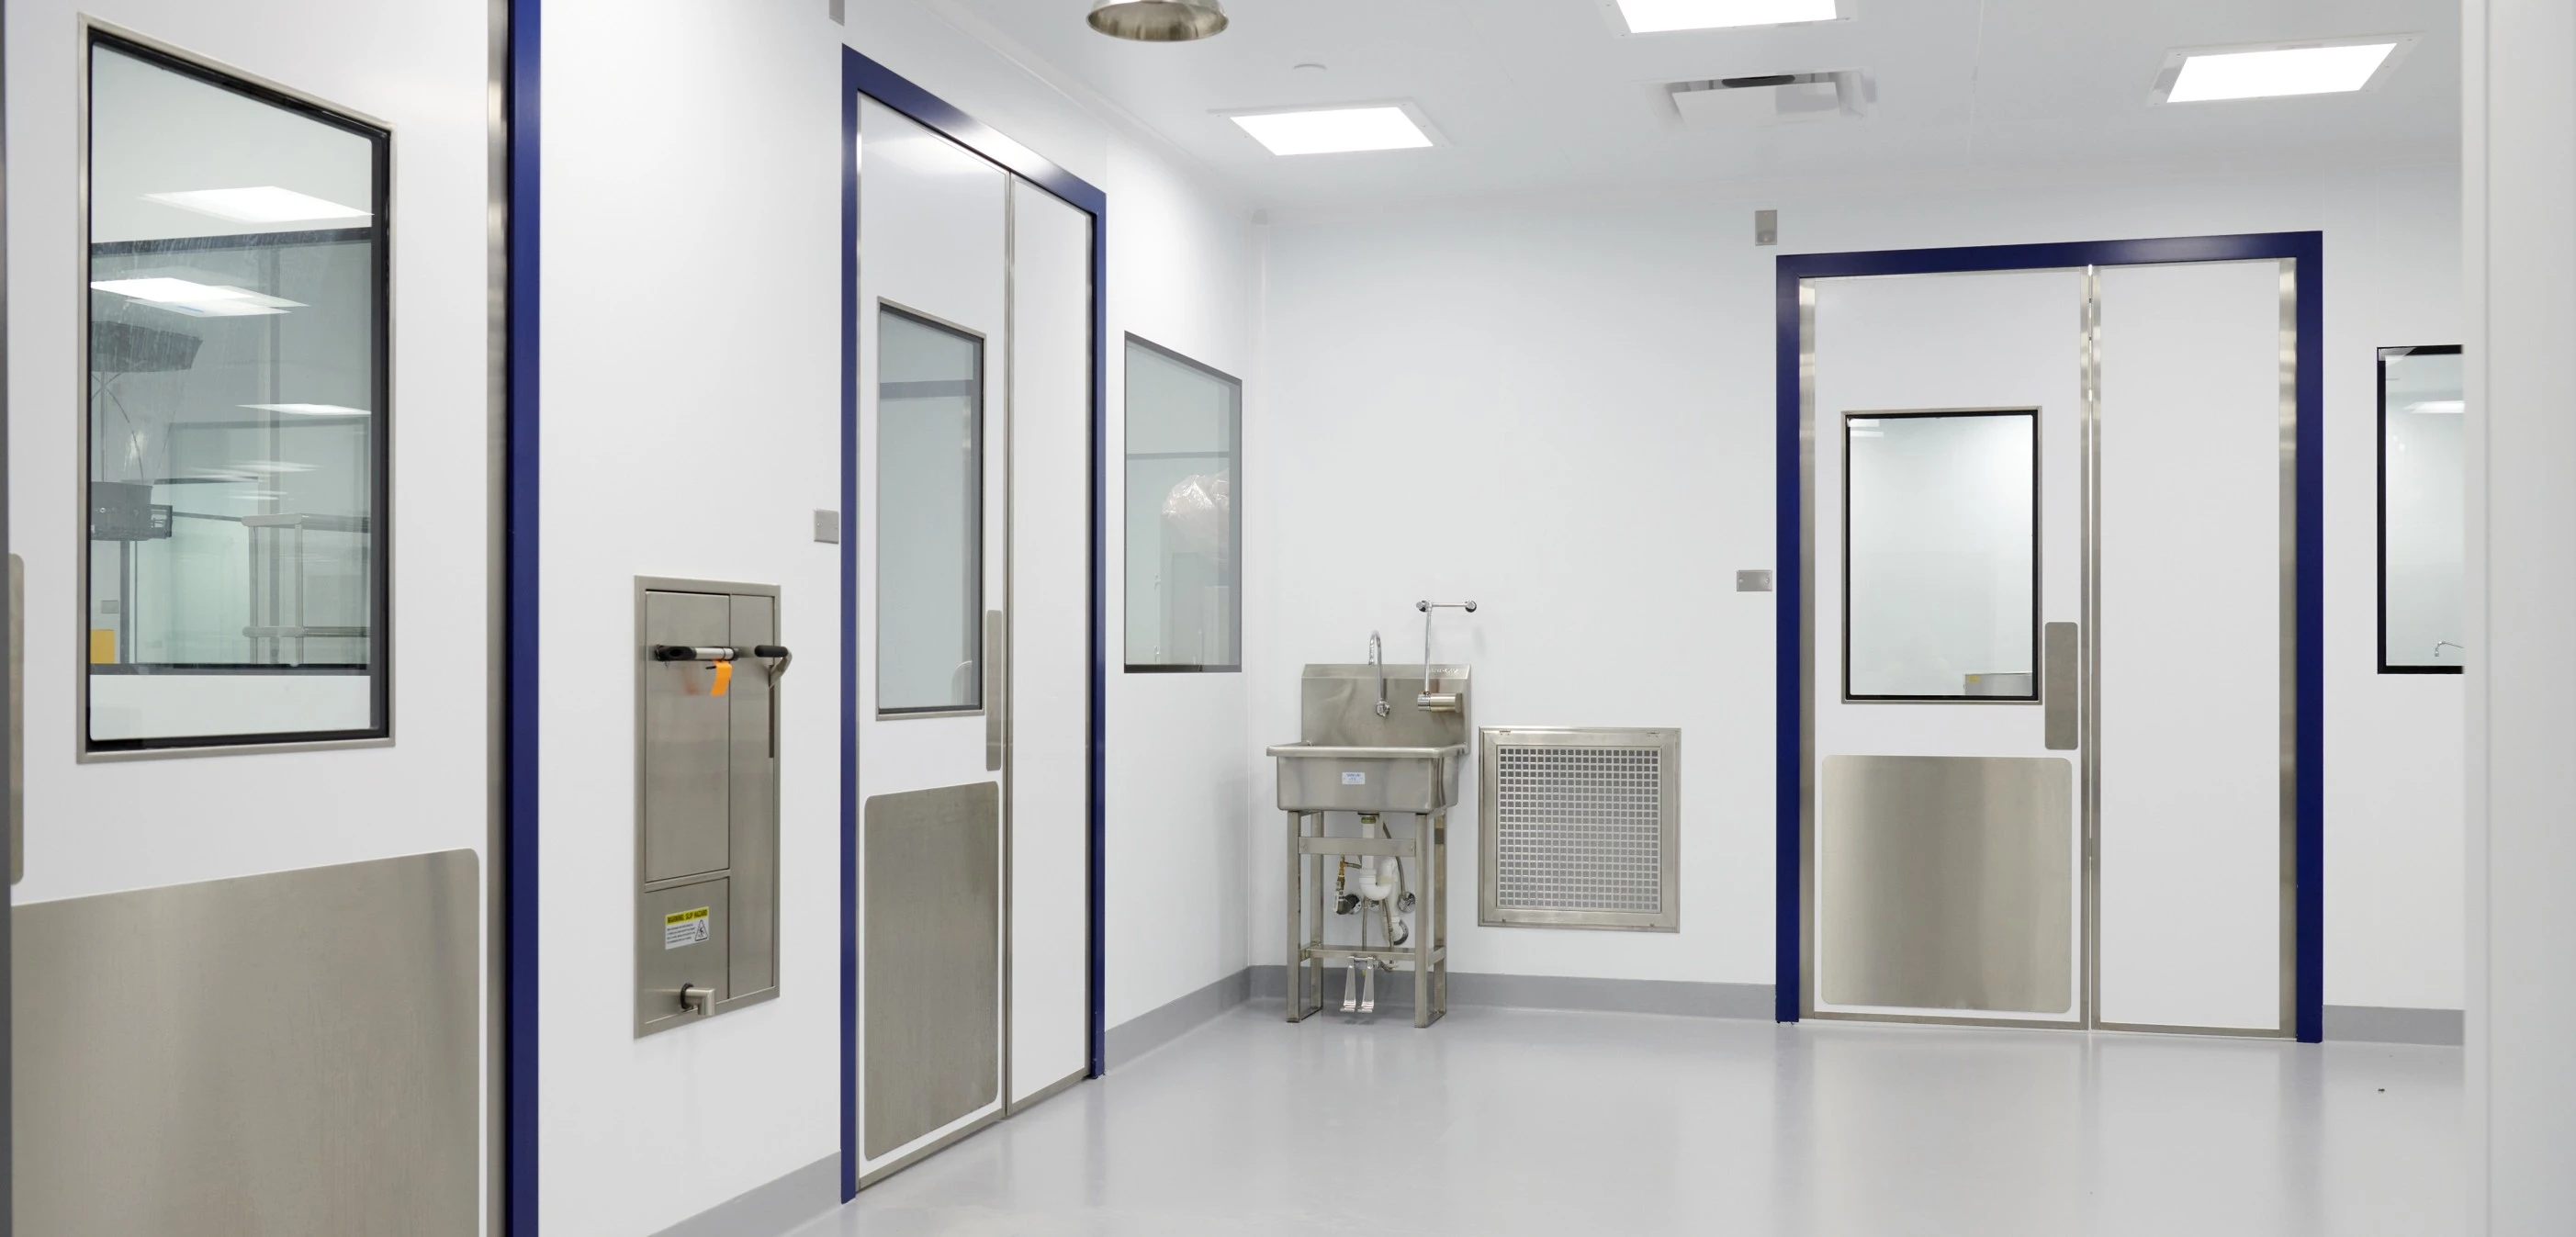
CleanSpace manufactures the controlled environment it engineers. Wall panels, ceiling systems, doors, windows, glass assemblies, interlocks, utility panels, lighting integrations, stainless components and accessory systems are coordinated directly with the project design and performance requirements.
That removes a critical handoff between the engineer and the product manufacturer. Openings, reinforcements, cutouts, panel dimensions, support conditions and component interfaces are resolved before production release. Manufacturing information comes from the coordinated design, not from a later interpretation of construction documents.
Direct manufacturing control also gives the project team visibility into:
- Material release
- Production status
- Quality reviews
- Delivery sequencing
- Installation requirements
- Schedule impacts
For executive leadership, that draws a clear line between committed capital and physical progress. Every material is tied to an engineered requirement, a construction sequence and a project milestone. That reduces the risk of buying ahead of design resolution, discovering fabrication conflicts in the field, or carrying schedule exposure because a critical component was treated as a separate purchase.
Installation Risk Is Reduced Through Self-Performance
A well-manufactured cleanroom system can still fail if the installer does not understand the engineering intent, assembly tolerances, sealing requirements or sequence of work.
CleanSpace installs its own systems with direct field supervision and its own skilled tradespeople. The installation team stays connected to the engineers and manufacturing personnel responsible for the system. Field questions do not travel through a distributor, an outside installer, a manufacturer and a consultant before they reach someone who can make a decision.
That connection protects:
- Wall alignment
- Ceiling loading
- Seals and coves
- Penetrations
- Door operation
- Component integration
- Cleanability
- Enclosure integrity
It also creates accountability. The organization that designed and manufactured the system stays connected to how it is installed. For the owner, that removes one of the hardest situations on any project: paying several firms to fix a problem created at the interface between them.
Commissioning Risk Is Addressed During Design
CQV cannot fix a facility that was never designed to be tested, accessed, balanced, maintained and qualified. An inaccessible balancing damper, an unresolved control sequence, too little maintenance clearance or a poorly coordinated ceiling penetration can turn into a commissioning problem long after the design decision was made.
CleanSpace brings commissioning and compliance requirements into design coordination. Test boundaries, pressure criteria, access points, alarm sequences, door interlocks, HEPA testing, recovery requirements, cleaning procedures and turnover documentation are all addressed before fabrication and construction.
Design the facility to be qualified. Don't built first and evaluated for qualification later.
When an issue appears during testing, the CQV team has direct access to the engineering, manufacturing and installation teams responsible for it. No separate contractual chain has to establish ownership before corrective action starts.
This is where facility delivery connects to the business plan. The value of the project is not realized at substantial completion. It is realized when the facility is qualified, compliant and producing. Every week between those two points is a week the owner's capital is deployed but not yet contributing to the business.
Operational Risk Continues After Turnover
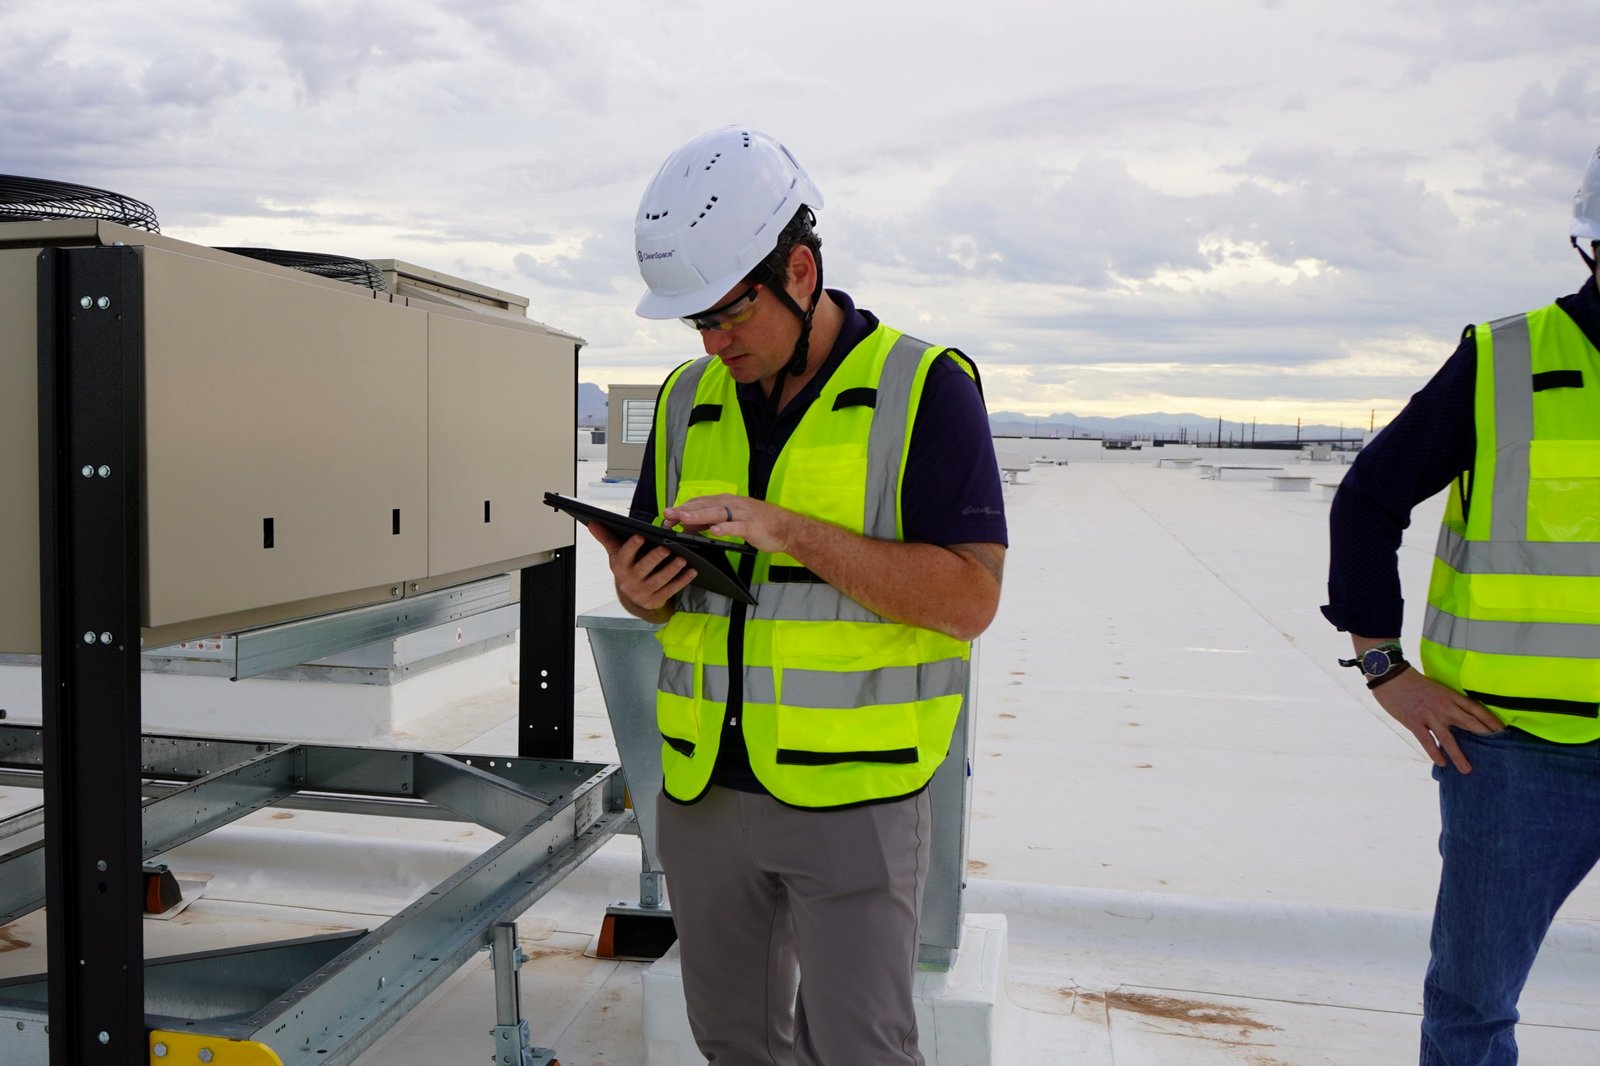
Facility readiness does not end when construction closes. The period right after turnover is when the facility becomes an operating GMP asset.
CleanSpace provides service and maintenance for the cleanroom enclosure, doors, interlocks, ceilings, components, testing and ongoing compliance. The team supporting the controlled environment keeps access to the original design intent, system information, installation history and commissioning requirements.
That continuity reduces a common post-project risk: an owner left holding a stack of closeout documents from firms that are no longer involved. Turnover is not the end of accountability. It is the move from project delivery to operational support, and no new organization has to relearn the facility.
Proven in Regulated Manufacturing
CleanSpace has applied this delivery model across pharmaceutical manufacturing, aseptic processing, biotechnology, vaccines, API, oral solid dose, containment, cell and gene therapy, CDMO, and 503A and 503B pharmacy facilities in the United States and Europe.
The recurring lesson: facility risk concentrates at the boundaries.
- Between engineering and construction
- Between manufacturing and installation
- Between controls and mechanical systems
- Between construction and CQV
- Between turnover and operations
- Between one contract and another
Every added handoff is another chance for information to be lost, responsibility to blur, or an issue to go unresolved. CleanSpace is structured to remove those boundaries, so the technical intent stays connected through the whole lifecycle.
The Executive Value of One-Source Delivery
For executive leadership, the value of the model comes down to five questions:
- Who owns the integration? One organization connects the technical requirements across disciplines and project phases.
- Who owns the interfaces? Issues between architecture, HVAC, controls, utilities, cleanroom systems, equipment, construction, and CQV are managed within one structure.
- Who protects the capital investment? Design, procurement, manufacturing, construction, and commissioning decisions stay tied to the intended operating outcome.
- Who owns readiness? The goal is not substantial completion. It is a qualified, compliant, operational facility.
- Who remains accountable after turnover? The relationship continues into service, maintenance, compliance, and operational support.
This is an accountability model, not just a delivery model. The fewer critical boundaries an owner has to manage, the fewer chances responsibility has to fragment.
The Executive Question
For a Head of Facilities, Project Executive, COO, CFO, Quality leader, or CEO, the most important question is not "Which contractor is responsible for this issue?"
It is: "Who owns the complete result?"
A GMP facility is not successful because the building was completed. It is successful when the capital investment becomes a qualified, compliant, operational asset that supports production and commercialization. CleanSpace is structured around that outcome.
One source. One accountable delivery structure. One continuous technical intent, from concept through commercialization and into operations.
What could the gap cost your project?
Run your numbers with the CleanSpace Cost of Delay Calculator and see what the time between completion and production is worth.